- -10%
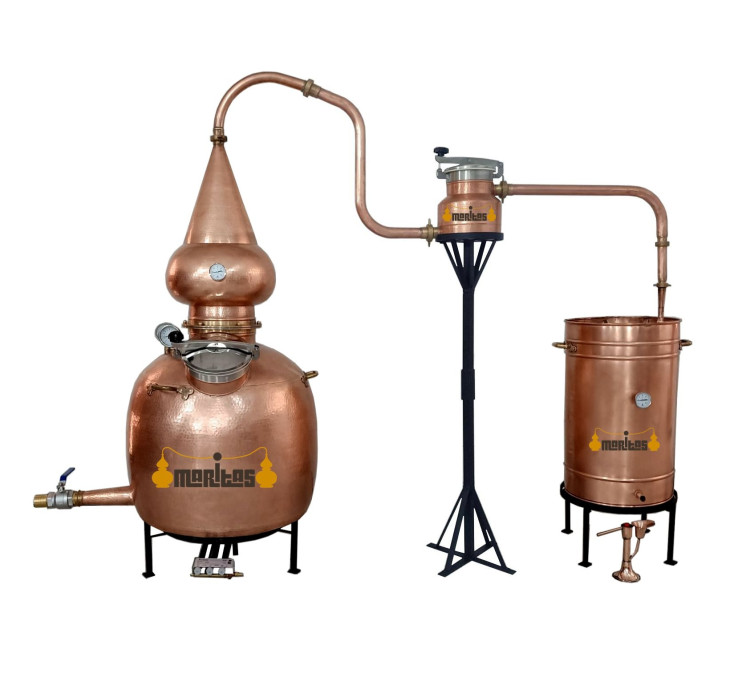


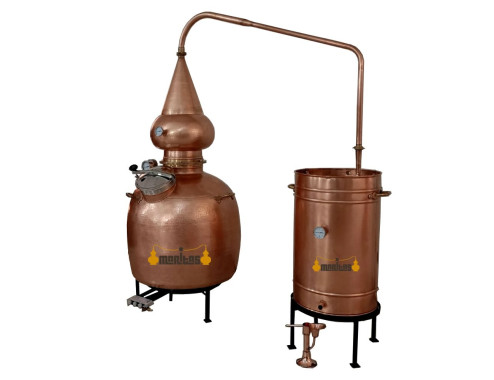
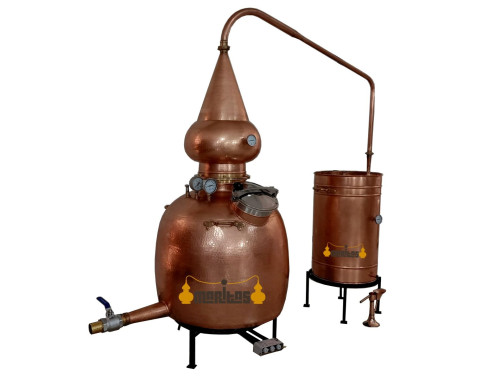
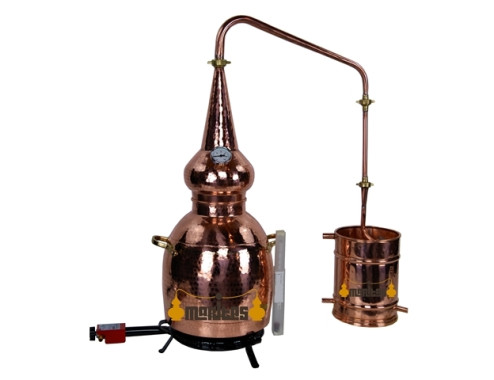
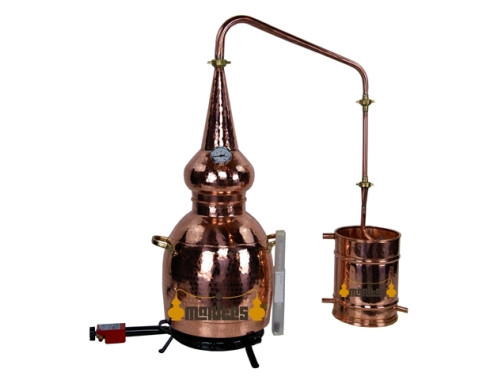
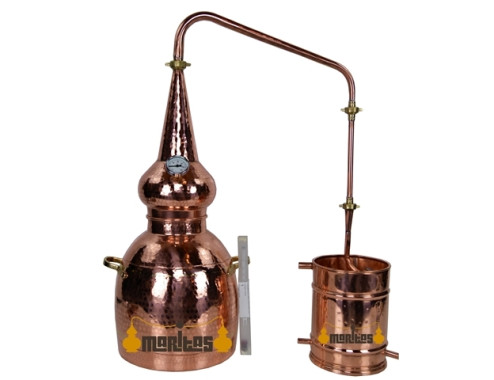
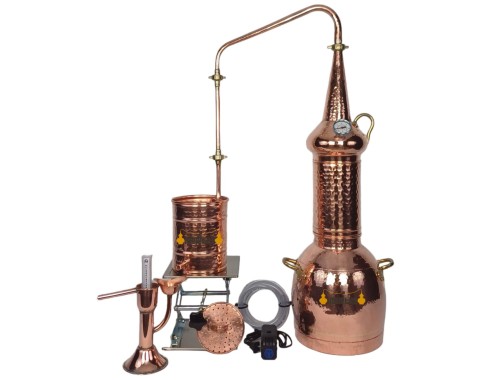
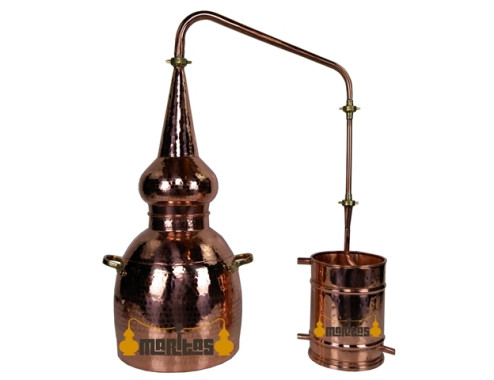
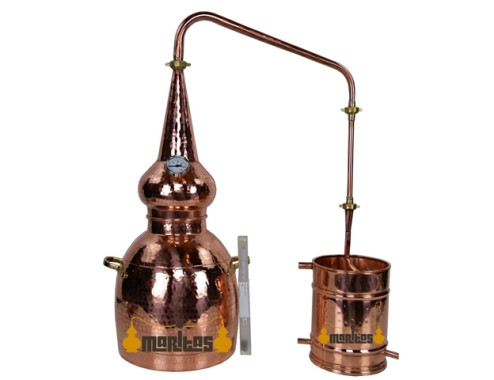
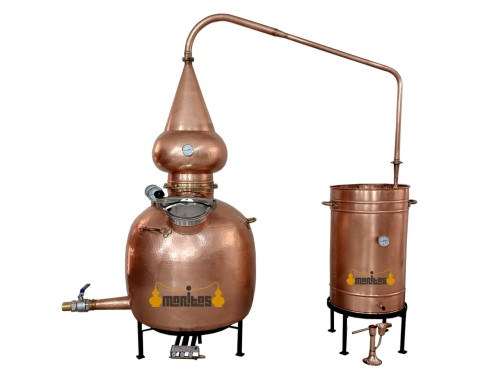
🥃 The 100L PROFESSIONAL Whisky Still + GIN BOX is designed for distilling gin, whisky and rum from fermented grain washes, fruit musts and molasses.
⚗️ Usable capacity: 100 litres (110 litres total capacity). Approximate yield of 10–15 litres per run with a wash at 10% ABV.
🔨 Made from 2 mm thick hammered copper, with comprehensive instrumentation for monitoring the distillation process.
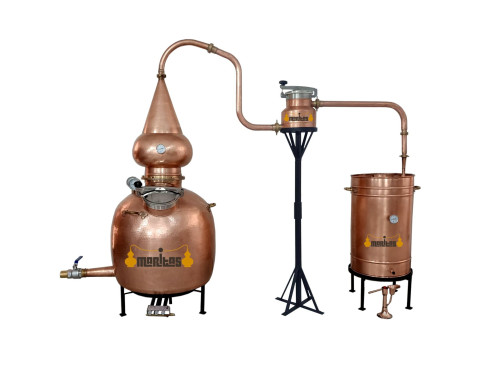
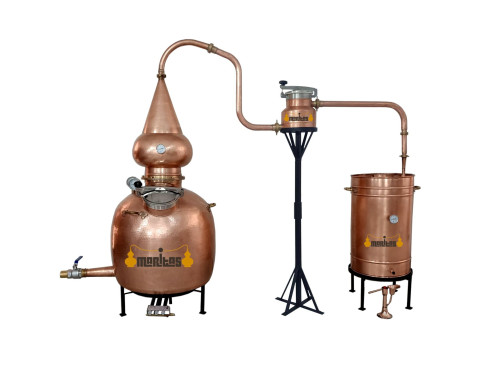
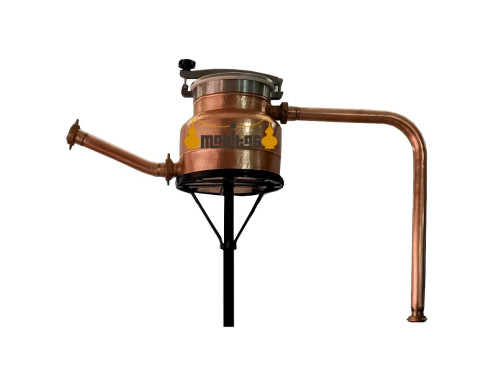
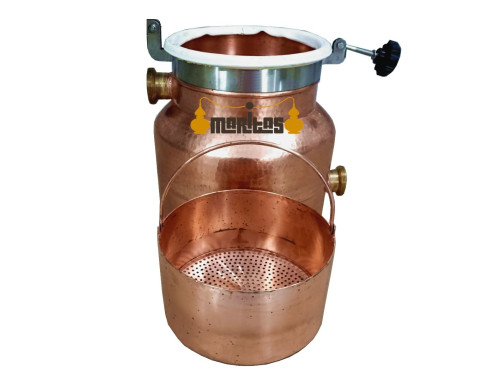
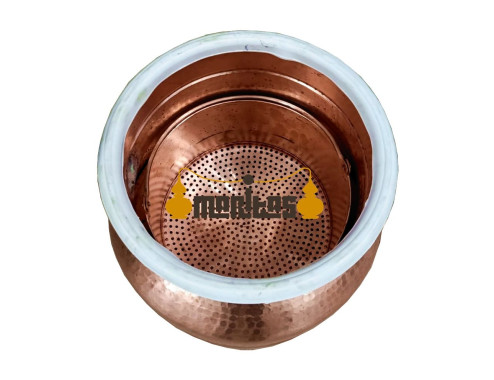
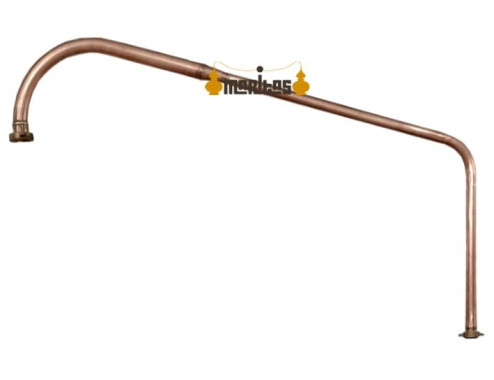
🌿 Includes a GIN BOX with a botanicals basket and a transfer pipe for distilling without it.
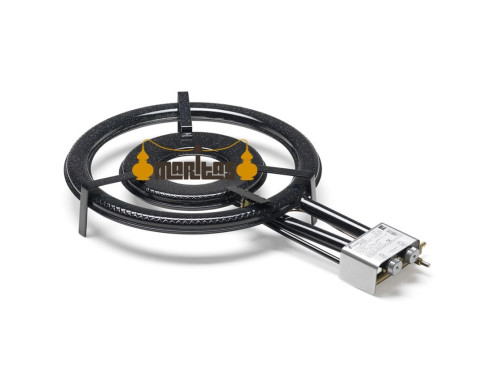
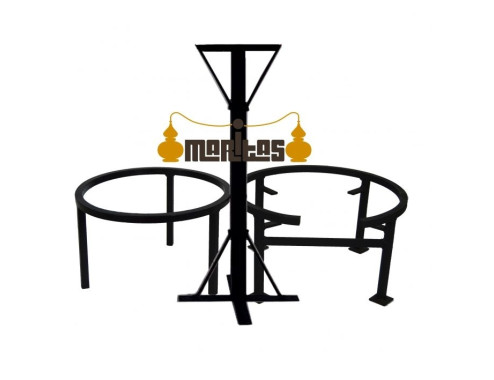
🔥 Includes a 46 cm professional gas burner and iron support stands.
✨ Made to order
📩 Request your personalized quote
⏱️ Check delivery times

Security Policy

Delivery Policy

Return Policy
Introducing the 100L PROFESSIONAL Whisky Still + GIN BOX, a high-quality distillation unit designed for producing gin, whisky and rum. It is particularly suitable for working with fermented grain washes, fruit musts and molasses.
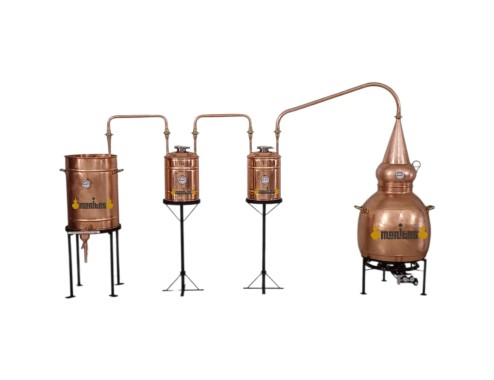
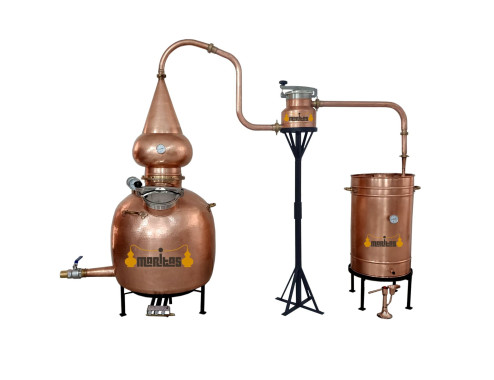
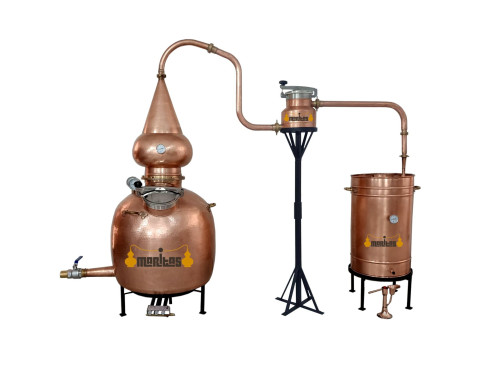
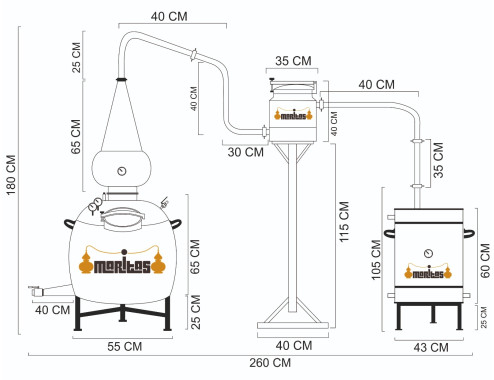
This model combines professional hammered copper construction with a GIN BOX fitted with a botanicals basket, allowing gin to be produced using either vapour infusion or maceration. It also includes a transfer pipe that allows the still to be used without the botanicals chamber, providing greater versatility for different distillation processes.
This model has a total capacity of 110 litres and a usable boiler capacity of 100 litres. The approximate distillation time is 3 to 4 hours.
Based on an initial wash with an alcohol content of 10% ABV, the estimated yield is between 10% and 15% of the usable capacity, equivalent to approximately 10–15 litres of distillate per run.
The final quantity obtained and the duration of each distillation may vary depending on the characteristics of the wash and the operating conditions.
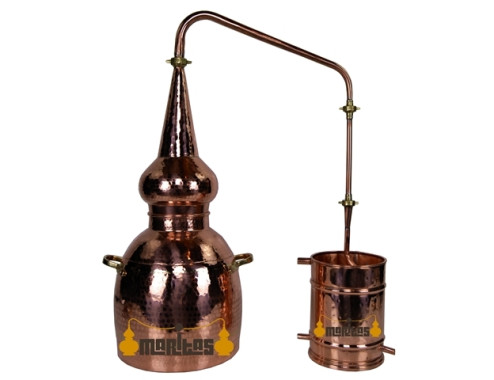
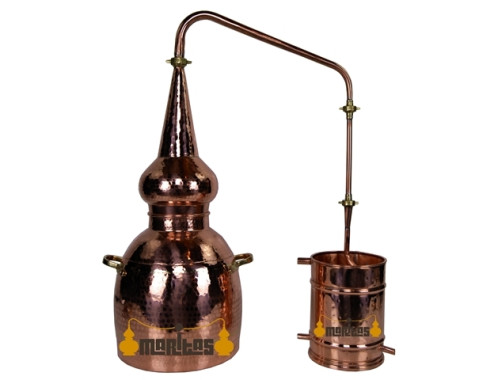
The still is made from 2 mm thick hammered copper sheet, a material traditionally used in distillation equipment. It features polished brass handles and nuts. All joints are soldered to provide a solid, robust and durable construction.
This model includes a GIN BOX with a botanicals basket, an accessory particularly suited to those wishing to produce gin using either vapour infusion or maceration.
The basket holds the botanicals used during distillation, allowing them to impart their characteristic aromas and flavours to the gin.
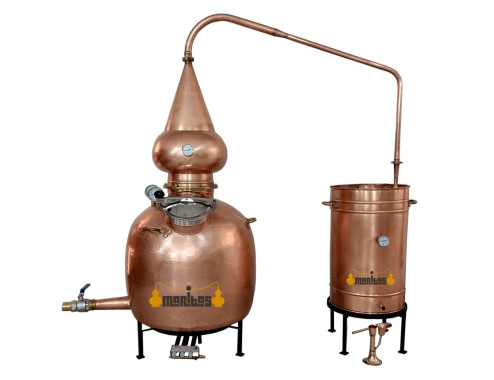
A transfer pipe is also included, allowing distillation to take place without using the GIN BOX. This means the equipment can be used either with or without the botanicals chamber, depending on the requirements of each process.
The equipment is fitted with several measuring instruments at different points, allowing the main variables to be monitored throughout the distillation process:
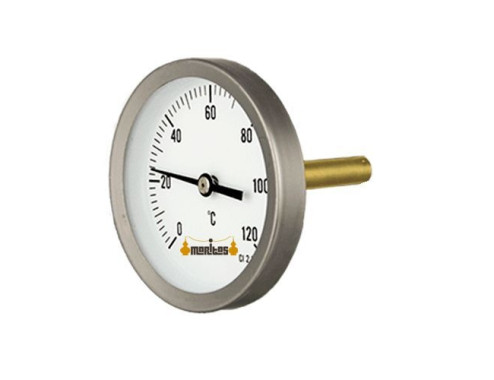
🌡️ Two large thermometers (0–120 °C): one is installed in the still head to monitor the temperature of the vapours as they pass through, while the other is fitted to the condenser to monitor the cooling system temperature.
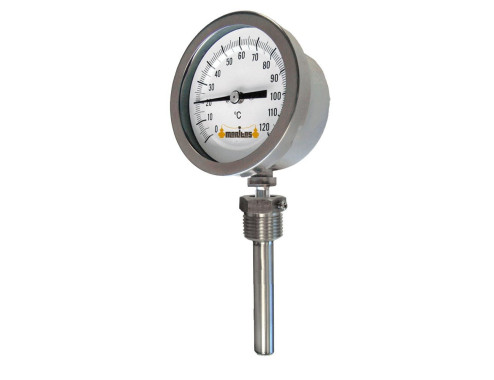
🌡️ Vertical boiler thermometer (0–120 °C): allows the temperature of the wash to be monitored during heating and distillation.
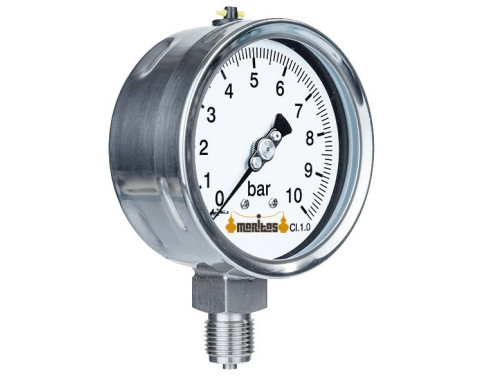
🔧 Boiler pressure gauge: allows the internal pressure of the equipment to be monitored.
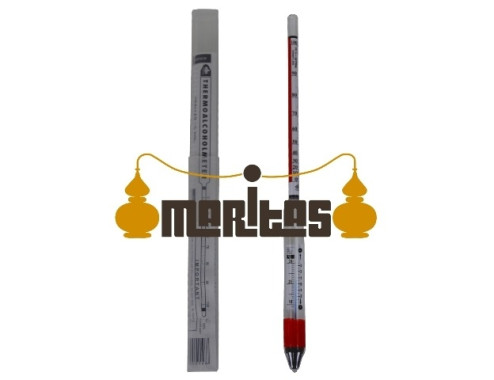
🍶 Alcoholmeter with thermometer: allows the alcohol strength of the distillate to be measured and its temperature to be monitored. A dedicated alcoholmeter stand is also included for convenient use.
The 100L PROFESSIONAL Whisky Still + GIN BOX incorporates several features designed to support operation and maintenance:
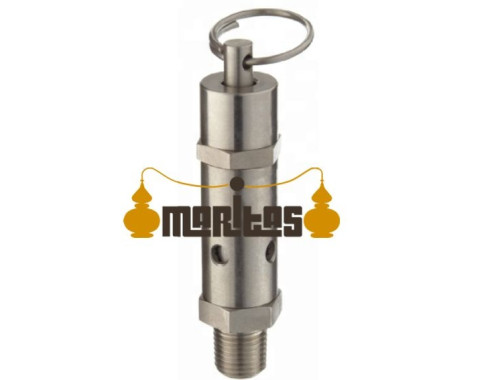
🔒 Boiler safety valve: fitted to help protect the equipment against excessive pressure.
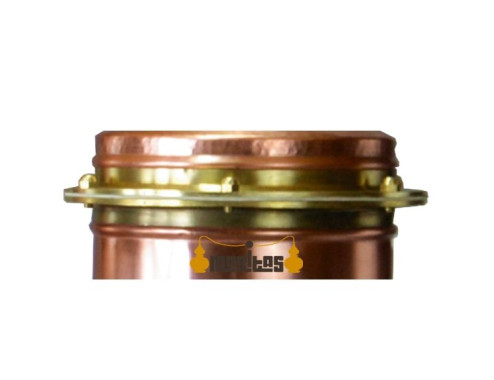
🔩 Brass connections between the boiler and still head: provide the connection and help ensure a secure seal between the two components.
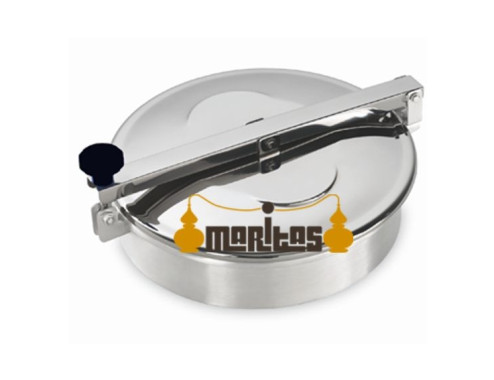
🚪 Boiler access door: made from stainless steel, it provides access to the interior for cleaning and maintenance.
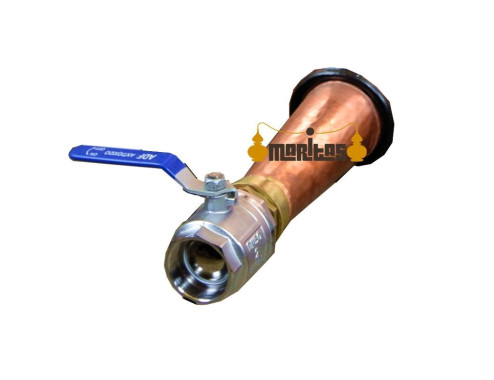
💧 2-inch drain pipe with valve: allows the remaining liquid to be drained from the boiler. It is made from stainless steel or brass.
The equipment includes a 46 cm diameter professional gas burner, compatible with butane and propane. A version suitable for natural gas is also available on request.
It is also supplied with iron support stands for the boiler, GIN BOX and condenser, allowing the different components to be positioned correctly.
The 100L PROFESSIONAL Whisky Still + GIN BOX is designed for those looking for versatile equipment for distilling gin, whisky and rum. Its 2 mm hammered copper construction, 100-litre usable capacity, comprehensive instrumentation and the option to use the GIN BOX or distil without it using the transfer pipe make it a professional, fully equipped solution for a range of distillation processes.
This model is made to order. The estimated manufacturing lead time is 30 to 45 days.

FICHA TÉCNICA
Download (676.63KB)TECHNICAL SHEET
Download (632.93KB)FICHE TECHNIQUE
Download (662.57KB)DATENBLATT
Download (655.97KB)SCHEDA DATI
Download (674.83KB)

🥃 The 100L PROFESSIONAL Whisky Still + GIN BOX is designed for distilling gin, whisky and rum from fermented grain washes, fruit musts and molasses.
⚗️ Usable capacity: 100 litres (110 litres total capacity). Approximate yield of 10–15 litres per run with a wash at 10% ABV.
🔨 Made from 2 mm thick hammered copper, with comprehensive instrumentation for monitoring the distillation process.
🌿 Includes a GIN BOX with a botanicals basket and a transfer pipe for distilling without it.
🔥 Includes a 46 cm professional gas burner and iron support stands.
✨ Made to order
📩 Request your personalized quote
⏱️ Check delivery times