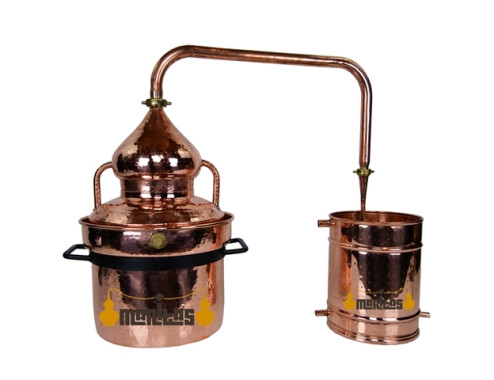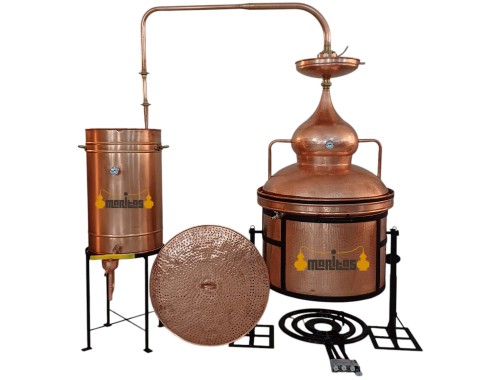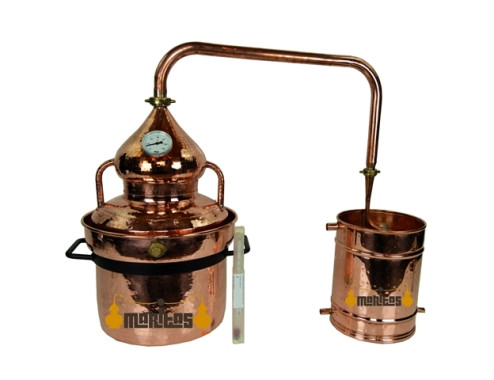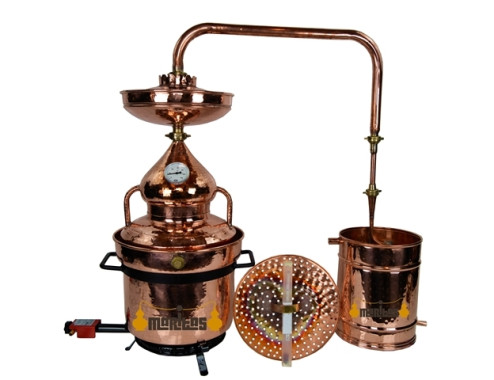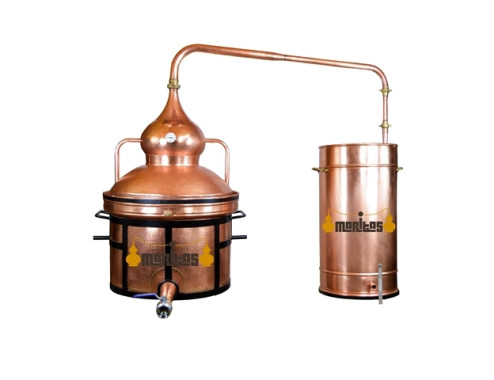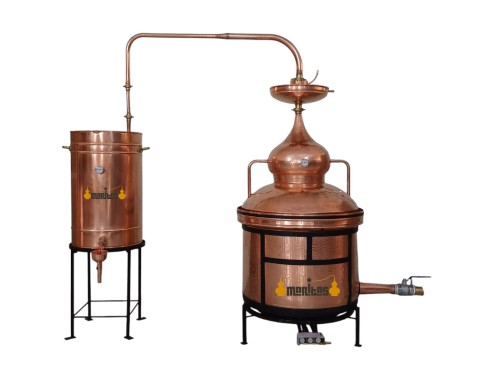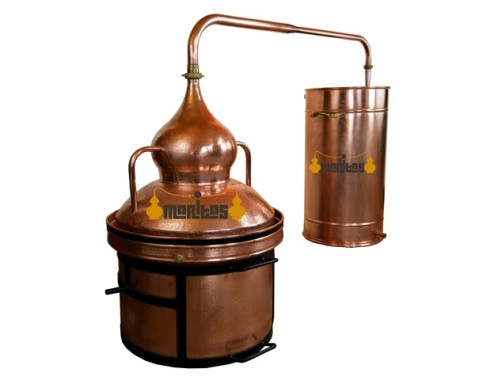


🥇 100-Litre Hydraulic Still for LIQUIDS
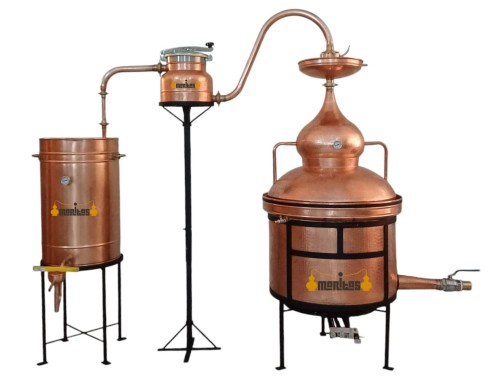
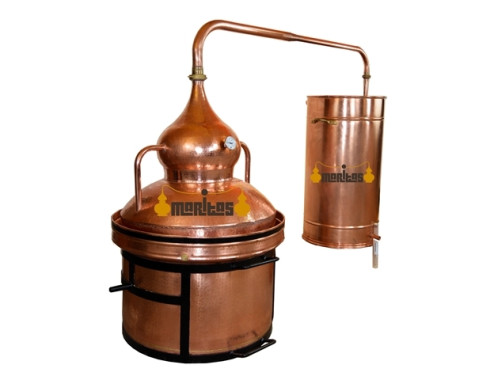
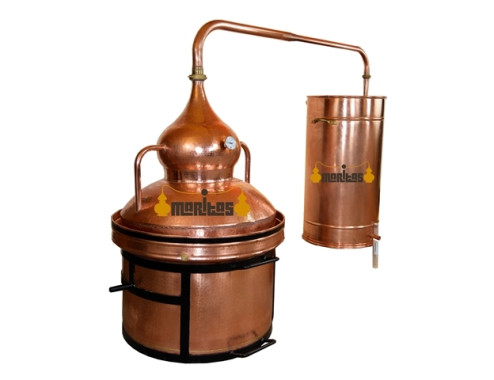
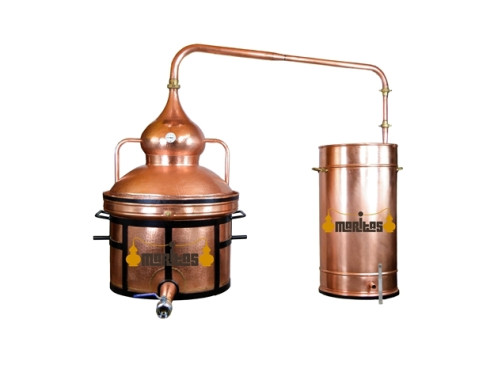
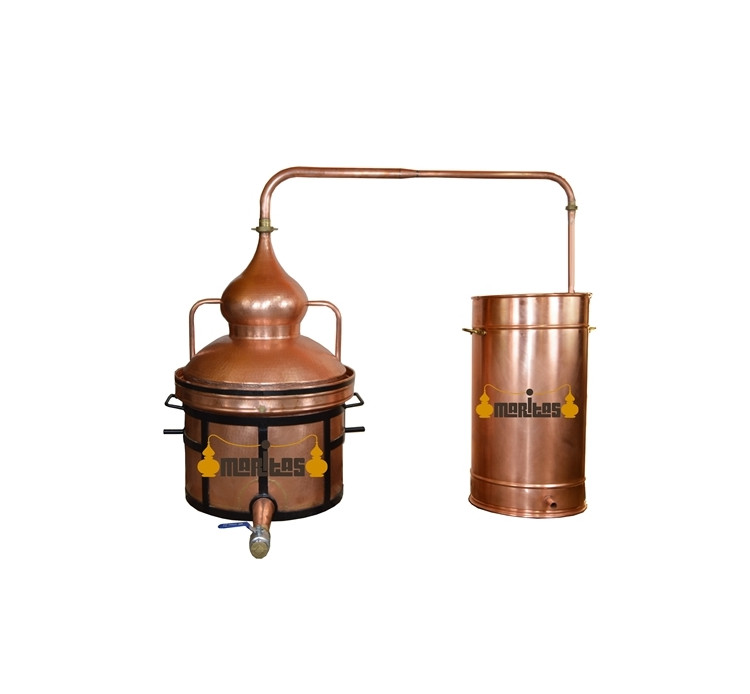
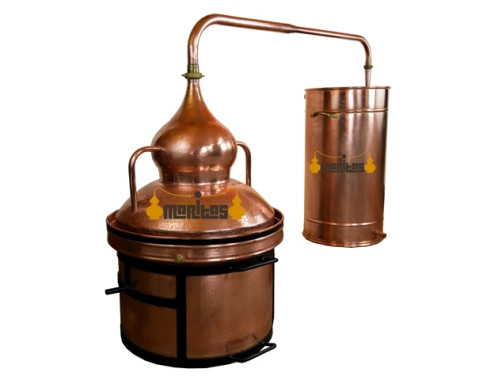
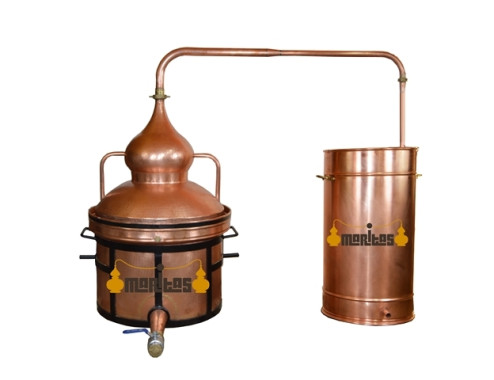
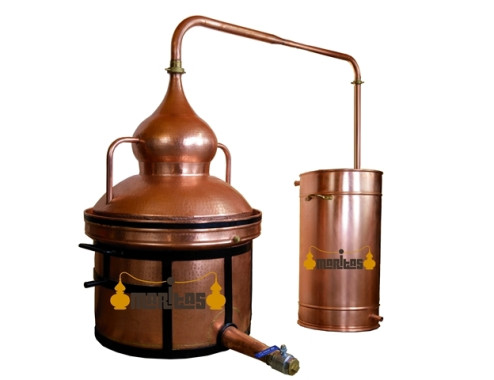
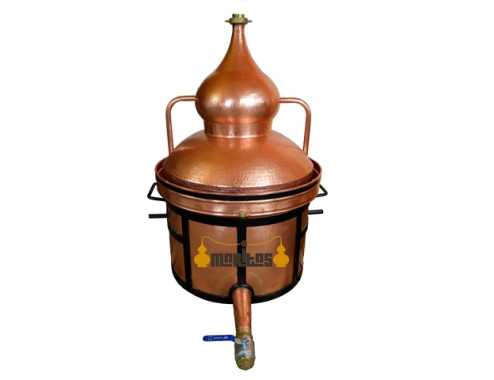
✨ Ideal for distilling fermented liquids such as spirits, wine and must. Made from 2 mm hammered copper, with a welded structure and iron reinforcements.
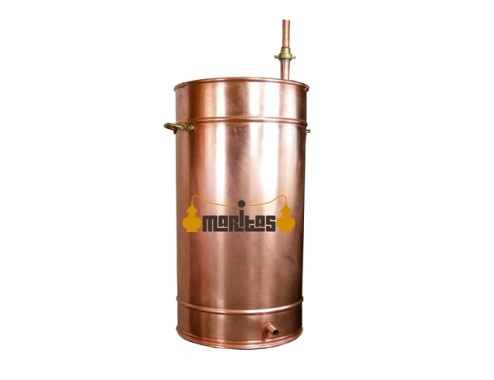
❄️ High-performance condenser.
🛢 Working capacity: 100 L · Time: 3–4 h
✨ Made to order
📩 Request your personalised quote
⏱️ Check delivery times

Security Policy

Delivery Policy

Return Policy
🥇 100-Litre Hydraulic Still for LIQUIDS
✨ Designed for alcoholic distillation of liquid ferments, combining high performance with excellent distillate quality.
The 100 L Hydraulic Still for LIQUIDS is a robust, durable piece of equipment designed to optimise the distillation of fermented liquids such as spirits, wine and must. Its reinforced construction and high-performance condenser help produce clean, aromatic distillates.
🛠 Premium construction
🔨 2 mm hammered copper: durable material traditionally used in distillation equipment.
🟡 Brass nuts and iron handles: sturdy components designed for long-term use.
🔗 Fully welded structure: built for strength and durability.
🧱 Iron boiler reinforcements: provide additional structural protection.
❄️ High-performance condenser
The condenser facilitates vapour condensation and optimises vapour flow throughout the process. This supports efficient condensation and helps produce a cleaner, purer distillate.
🔥 Capacity and performance
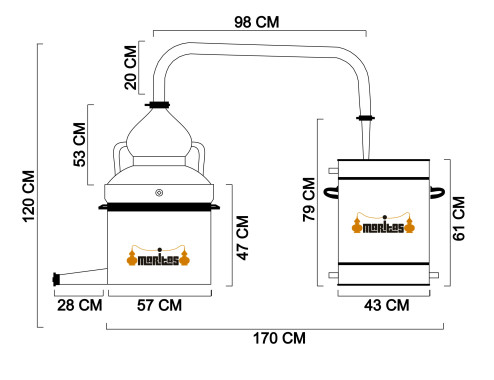
🛢 Total capacity: 110 litres
🧪 Working capacity: 100 litres
⏳ Estimated distillation time: 3–4 hours
📈 Indicative yield: 10–15% of working capacity, depending on the fermented liquid and operating conditions.
📊 Approximate output
For simple distillation without a rectifier, using a fermented wash at 10° alcohol:
➡️ Estimated output: 10–15 litres at approximately 45% ABV.
With rectification:
➡️ Estimated output: 8–10 litres at approximately 75% ABV.
These figures are approximate and may vary according to the initial alcohol content, type of ferment, operating method and distillation settings.
🧴 Process optimisation
This model is designed to combine capacity, durability and efficiency when distilling fermented liquids. Its reinforced construction, high-performance condenser head and safe discharge system support a practical and efficient distillation process.
✨ A robust, durable solution for those looking to optimise the distillation of fermented liquids.
FICHA TÉCNICA
Download (311.57KB)TECHNICAL SHEET
Download (258.74KB)FICHE TECHNIQUE
Download (305.98KB)DATENBLATT
Download (258.44KB)SCHEDA DATI
Download (265.69KB)

🥇 100-Litre Hydraulic Still for LIQUIDS
✨ Ideal for distilling fermented liquids such as spirits, wine and must. Made from 2 mm hammered copper, with a welded structure and iron reinforcements.
❄️ High-performance condenser.
🛢 Working capacity: 100 L · Time: 3–4 h
✨ Made to order
📩 Request your personalised quote
⏱️ Check delivery times